Installation, Welding & Daily Maintenance Guidelines
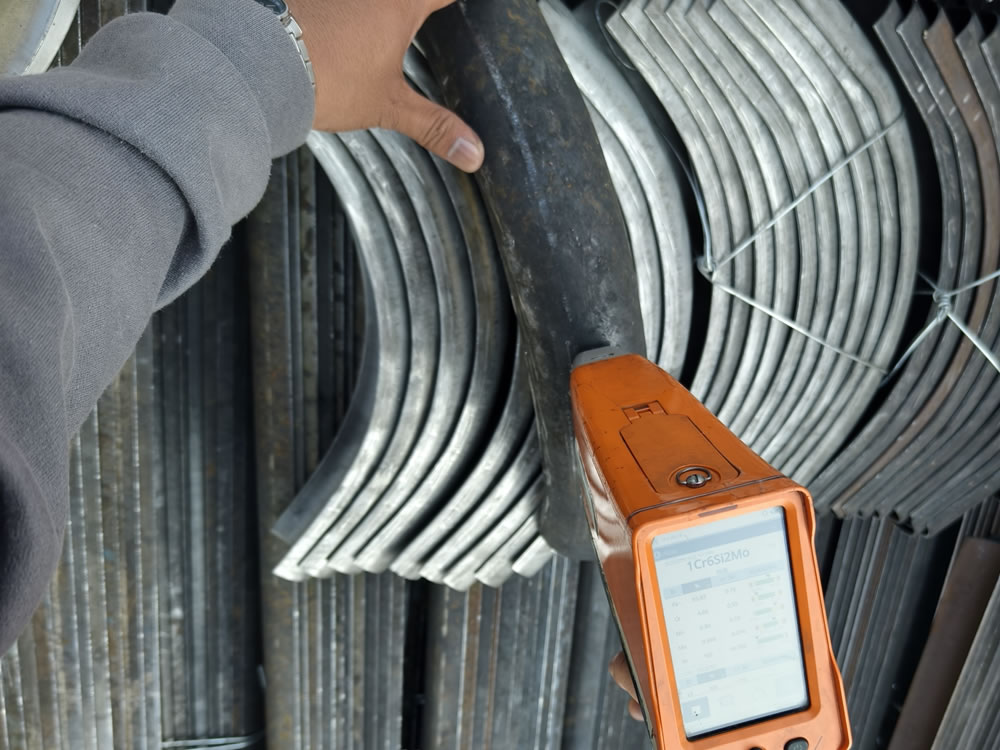
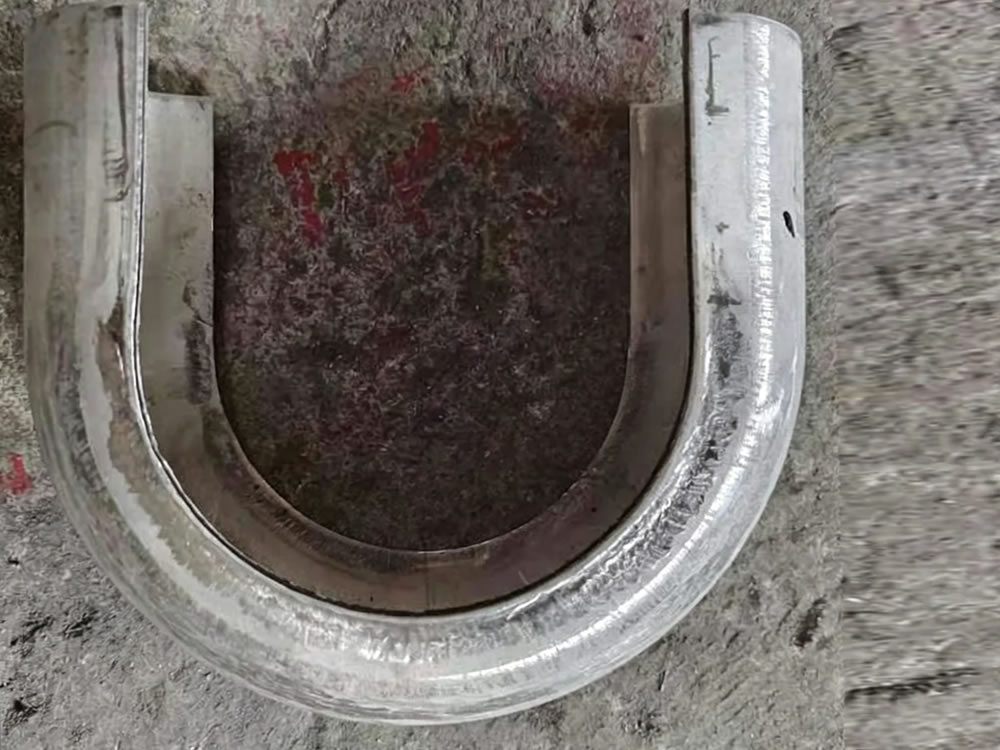
1Cr6Si2Mo heat resistant alloy has strict welding operation requirements to avoid crack defects:
Preheat workpiece to 300~400℃ before welding, select matching heat resistant alloy welding rod, implement slow furnace cooling after welding to eliminate welding stress and cold cracks.
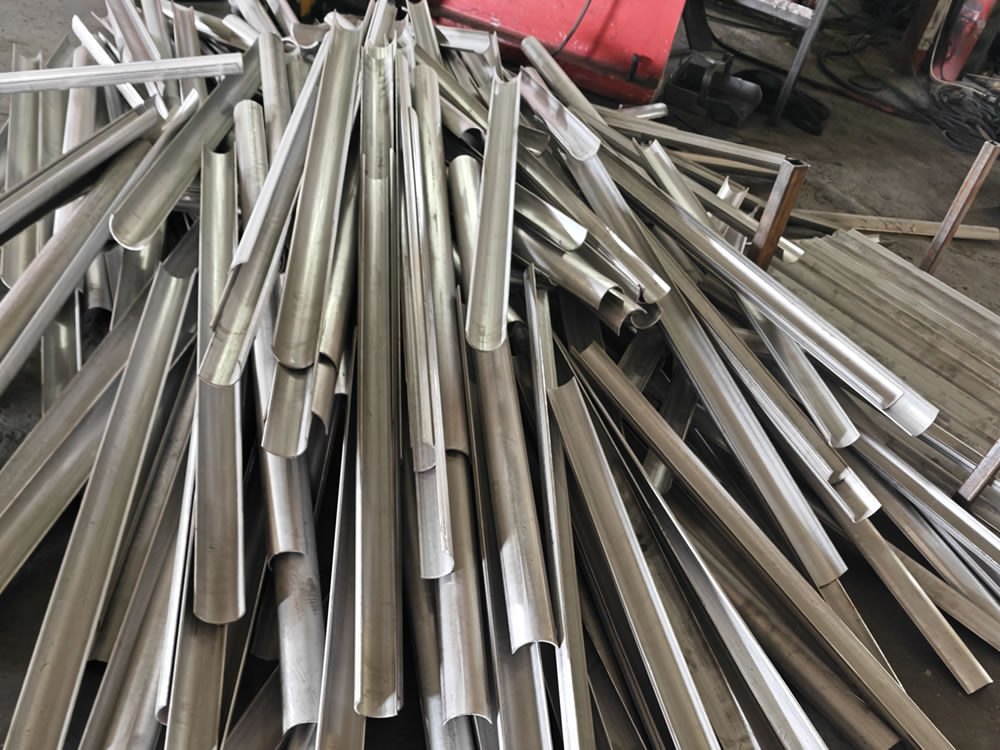
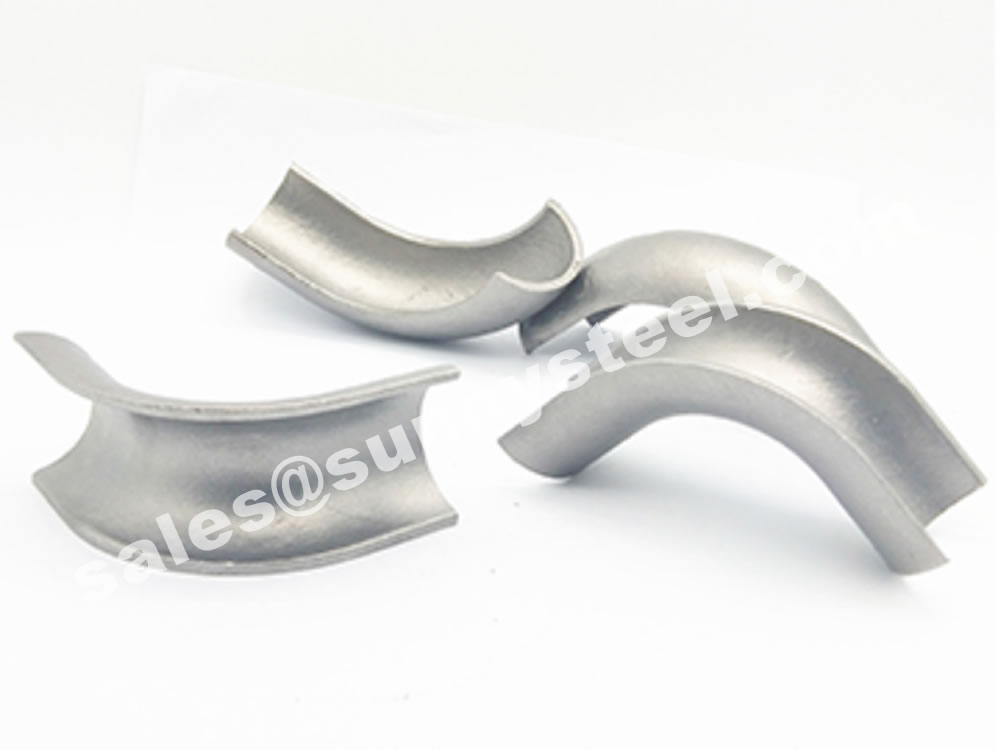
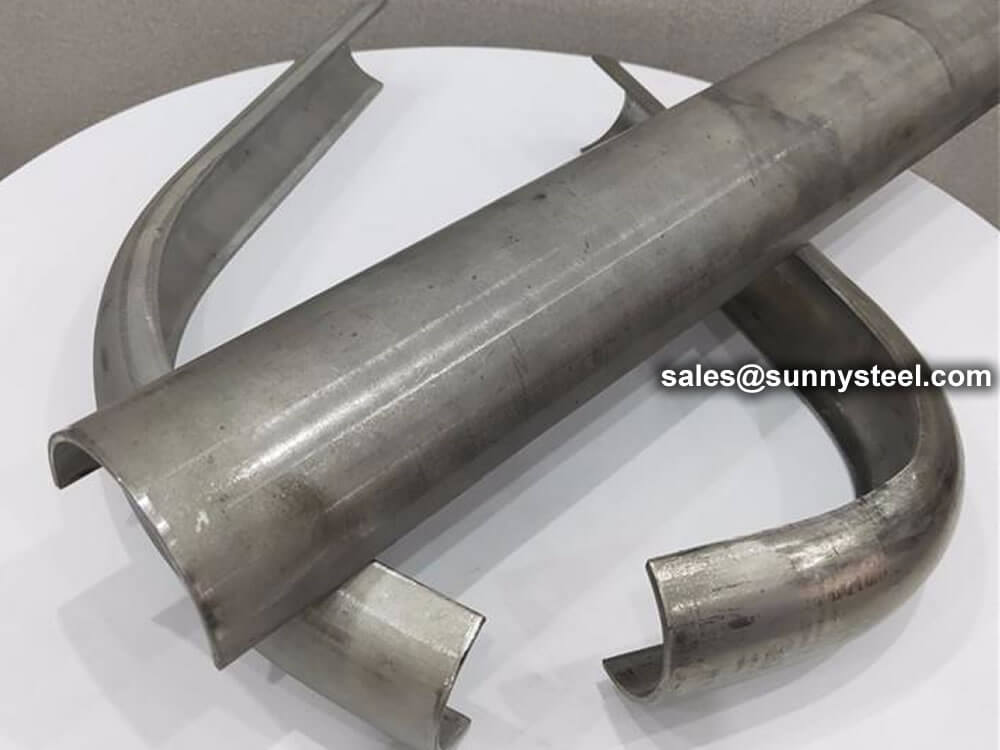
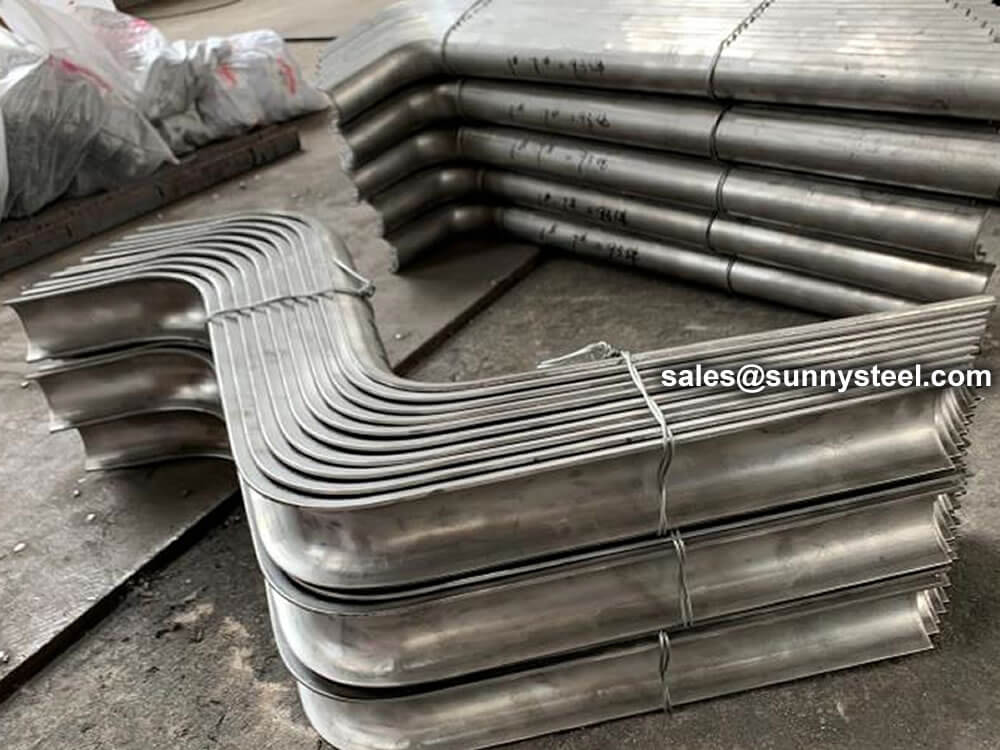
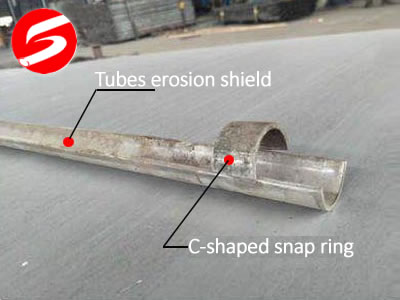
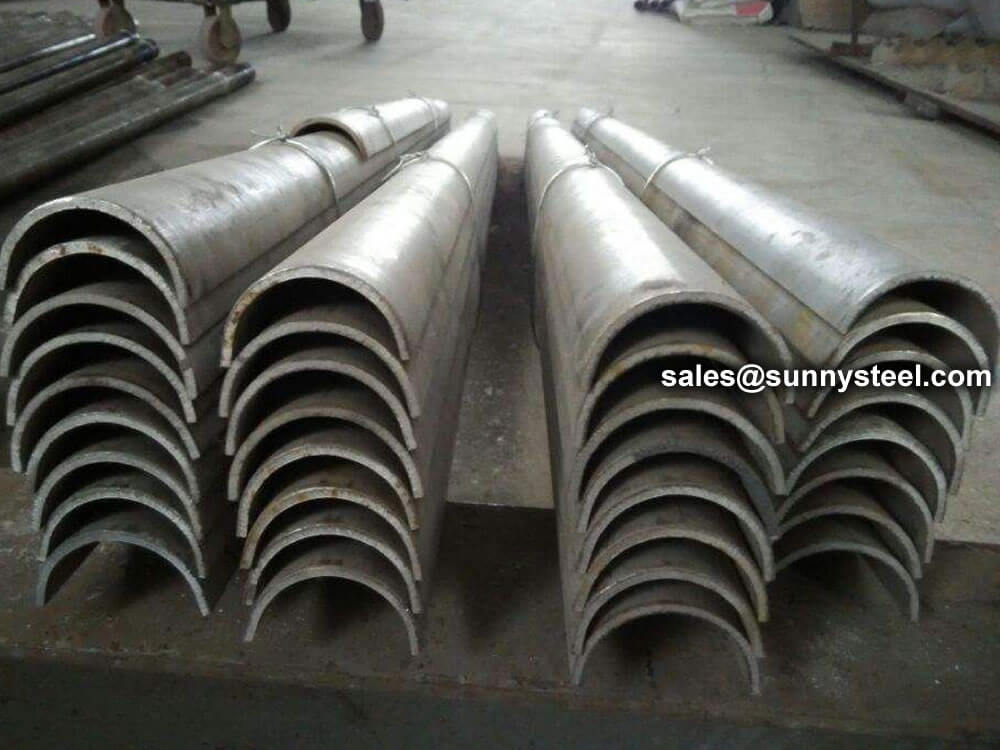
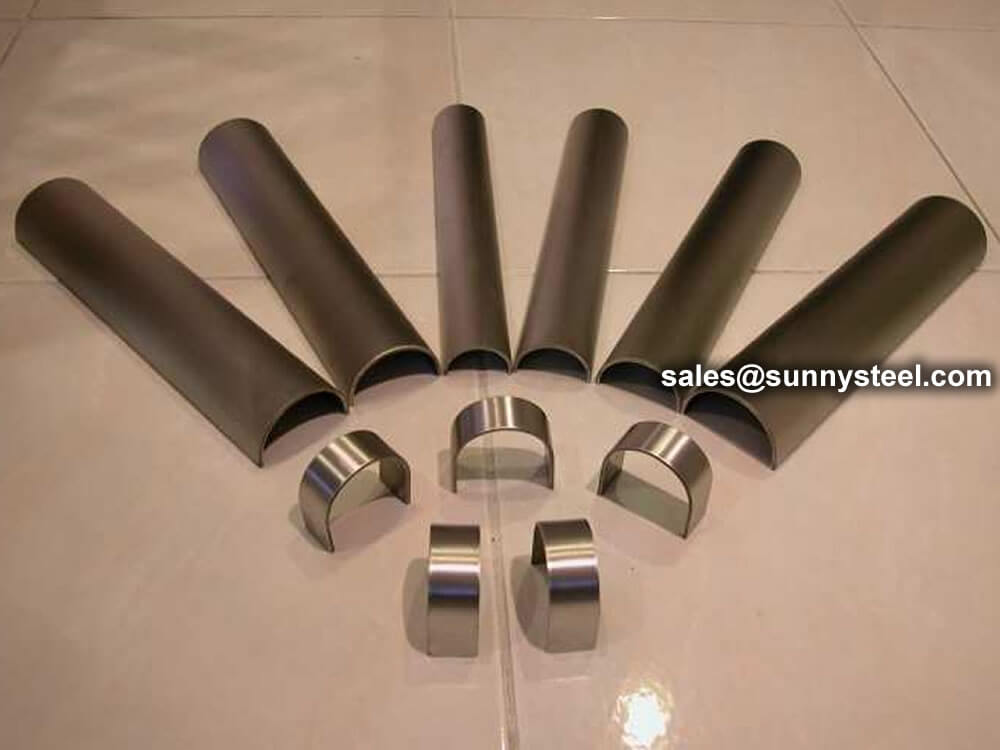
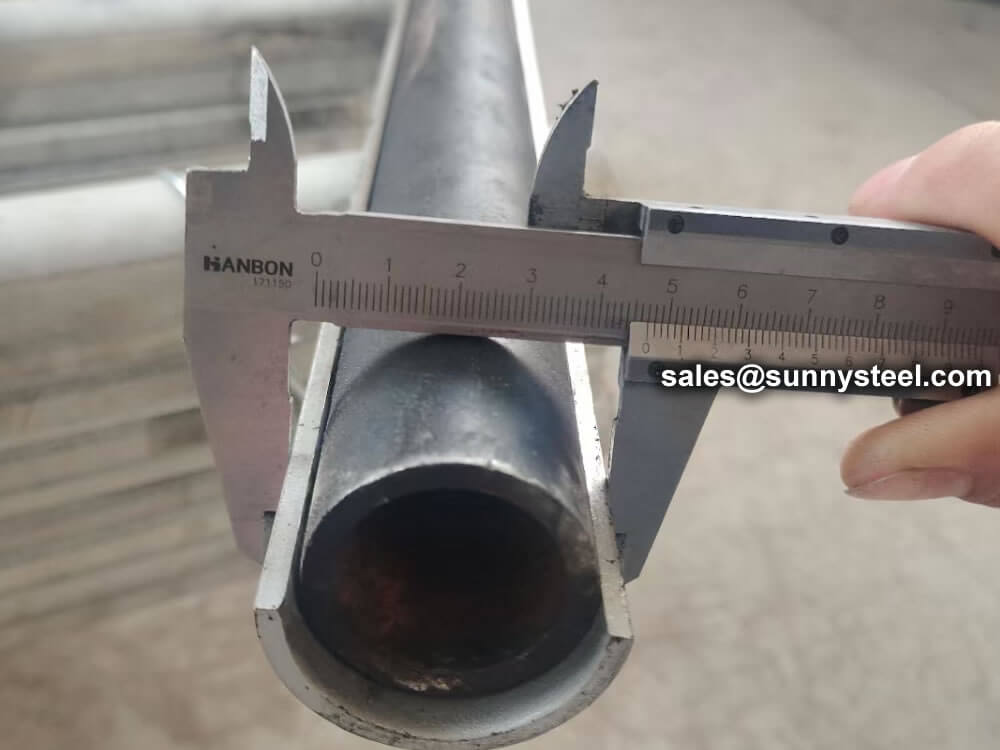
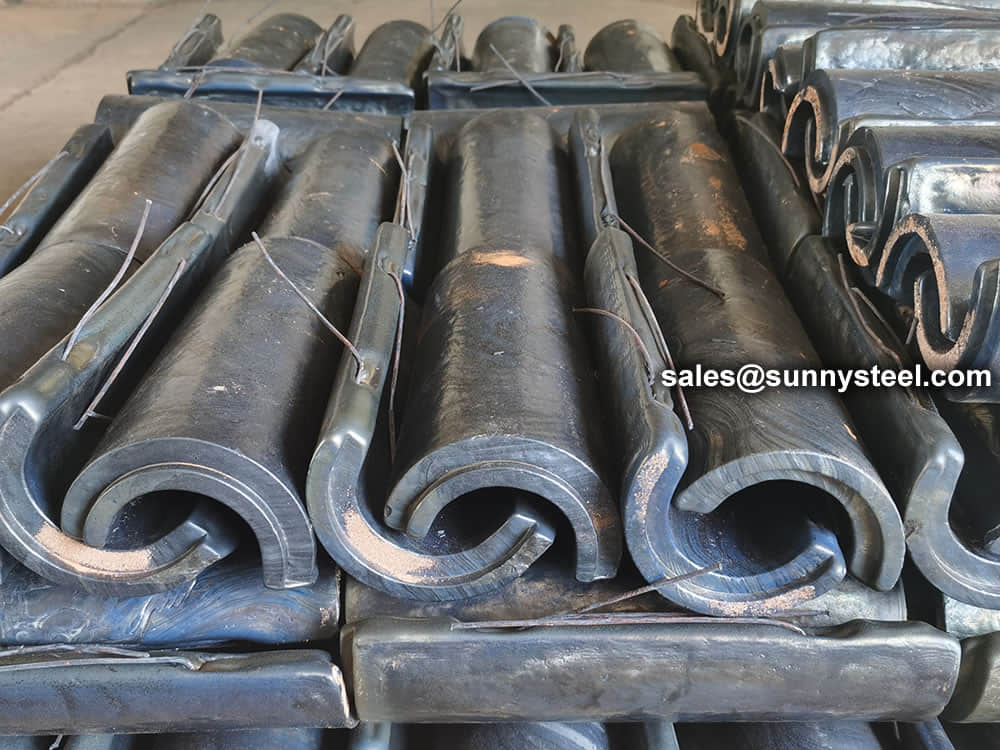
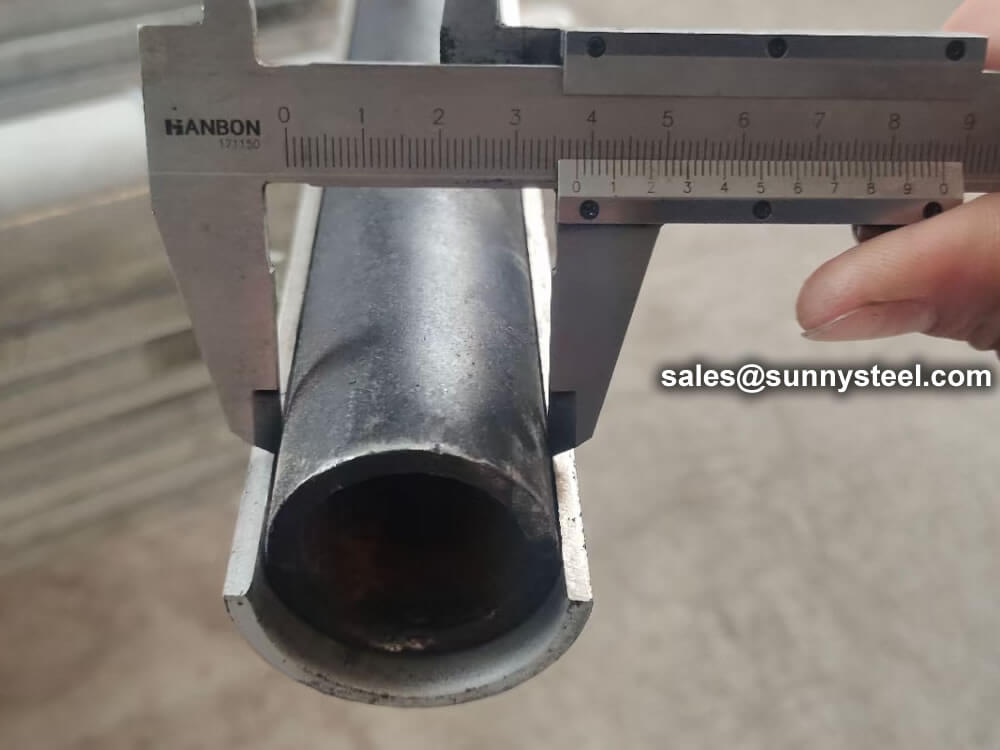
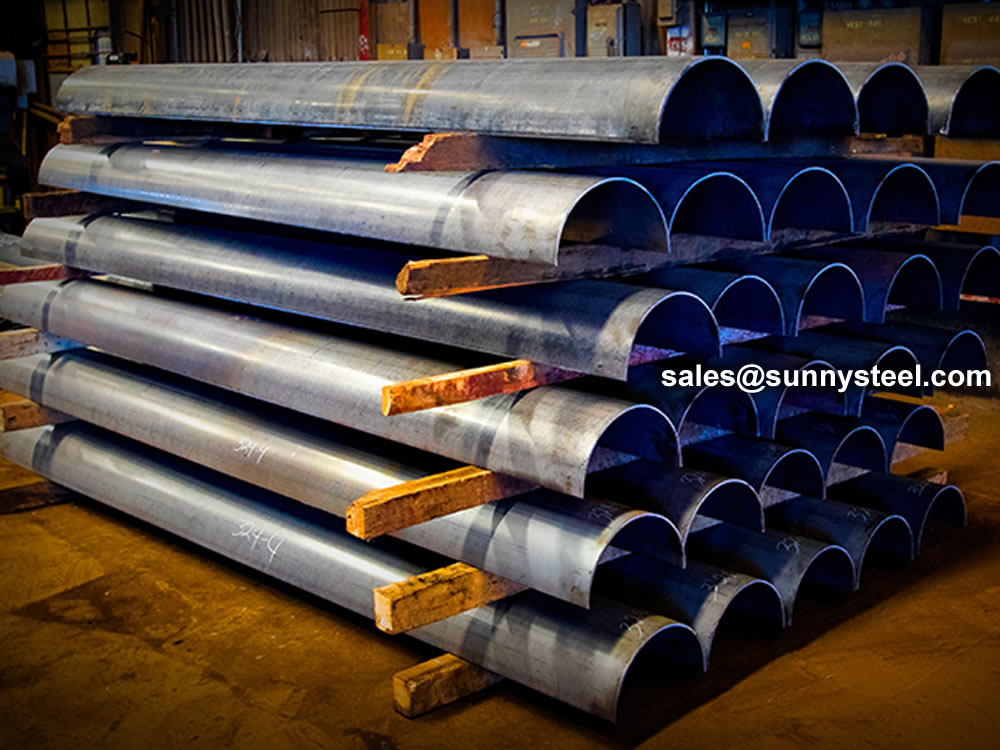
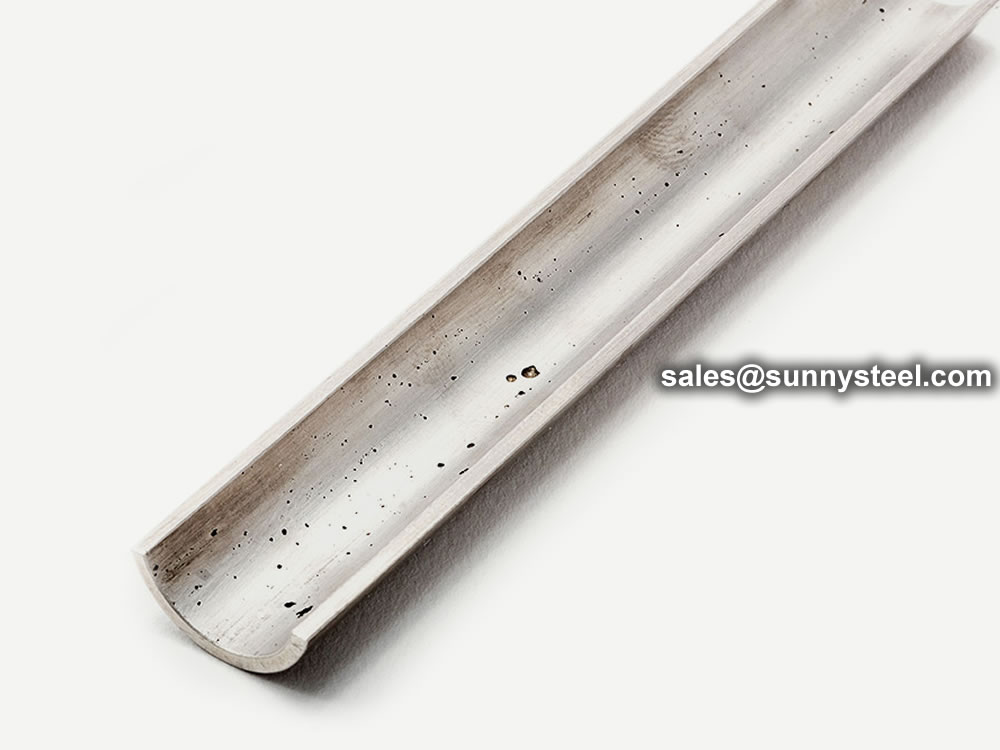
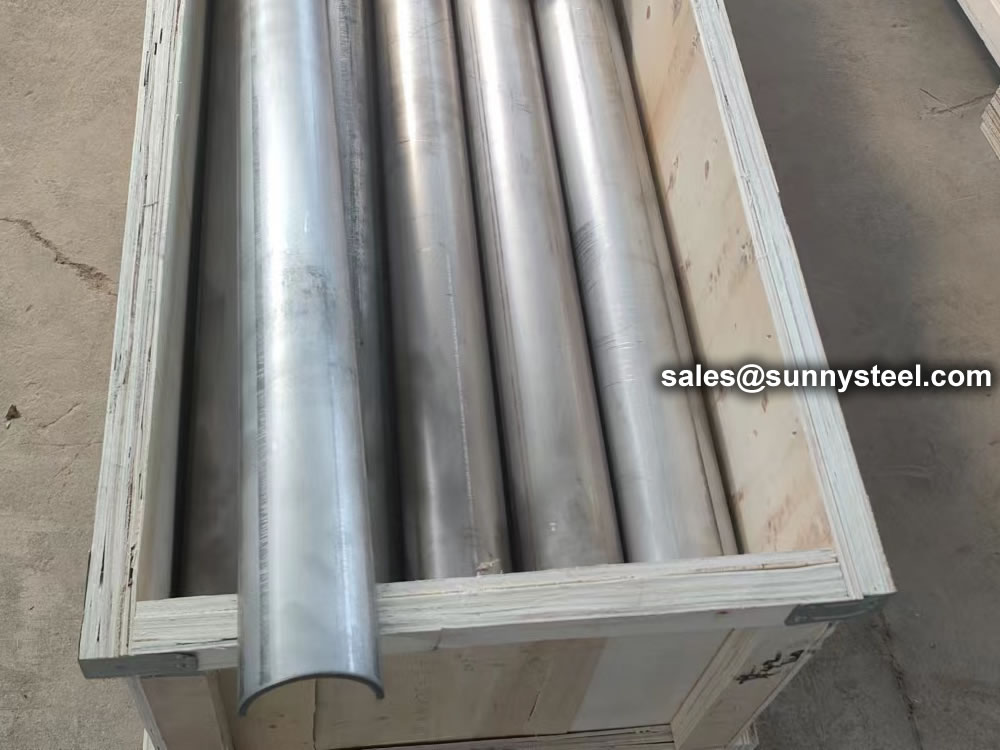
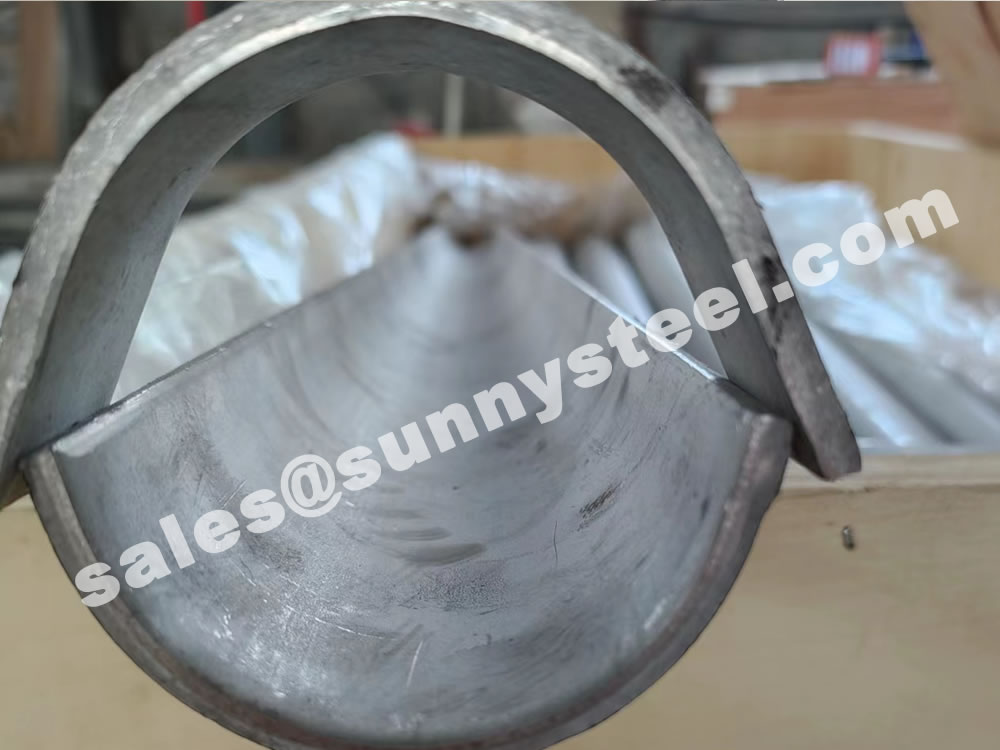
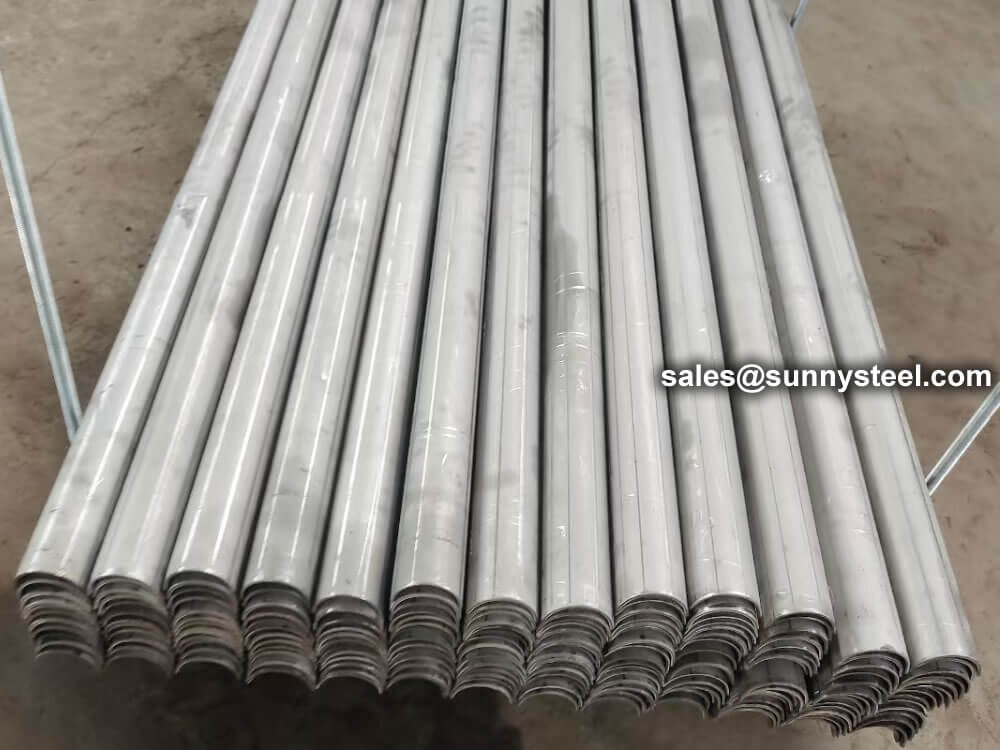
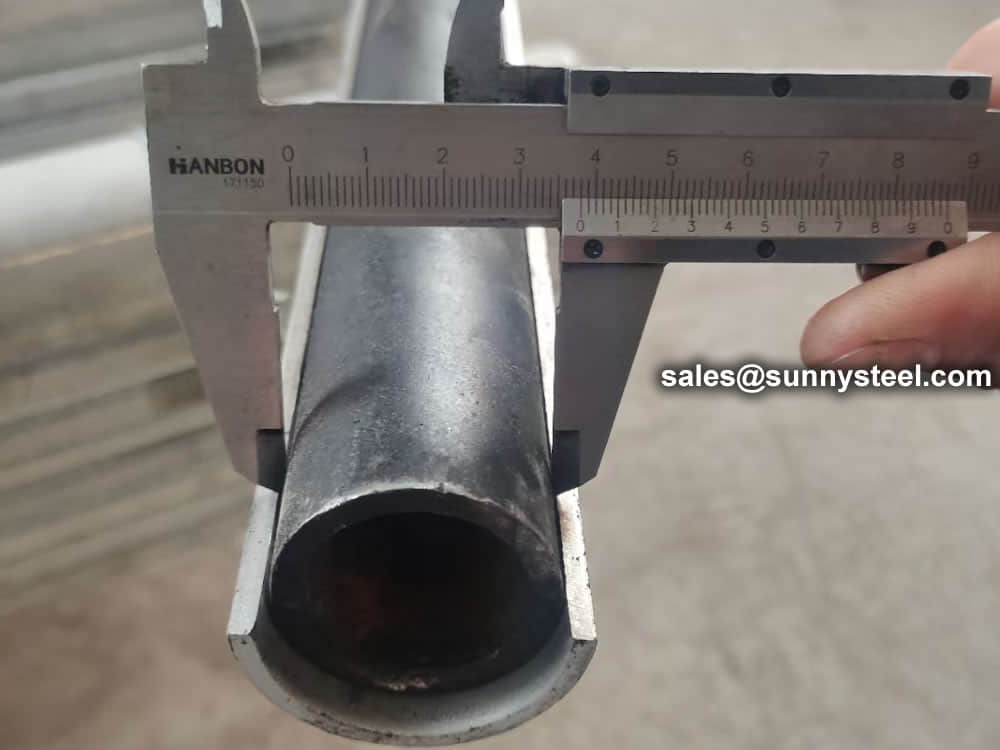
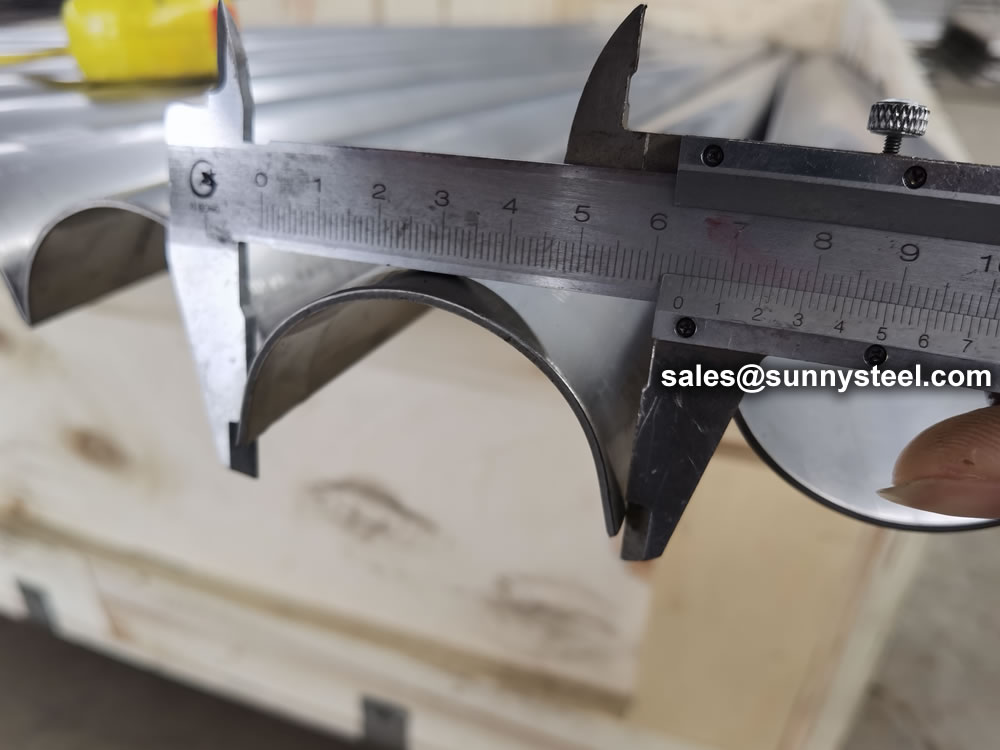
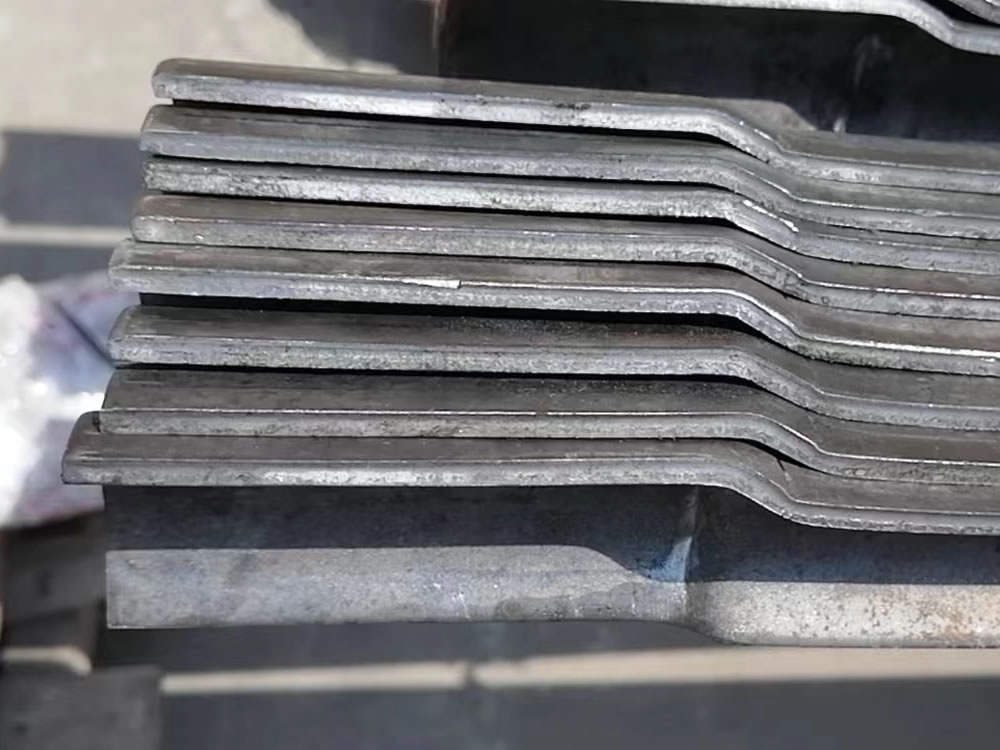
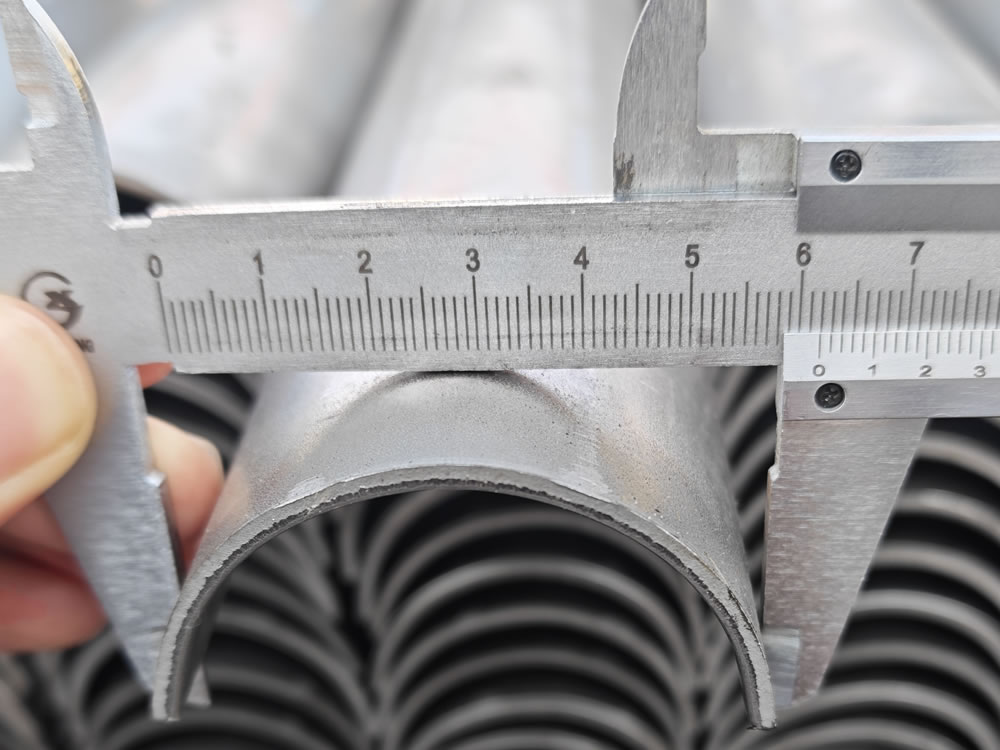
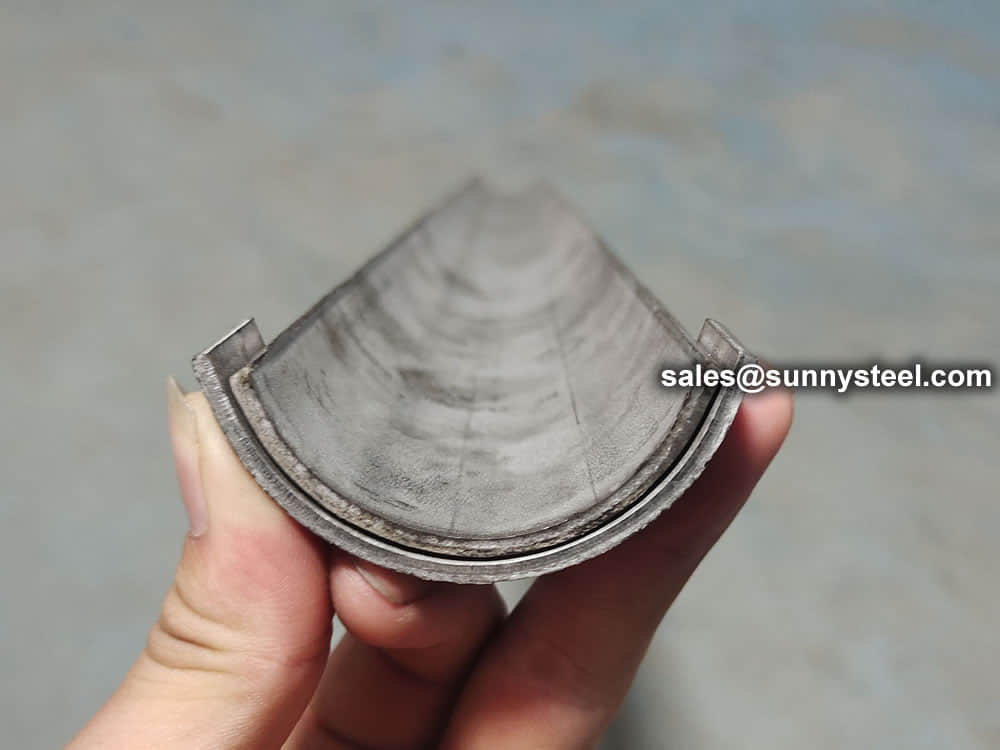
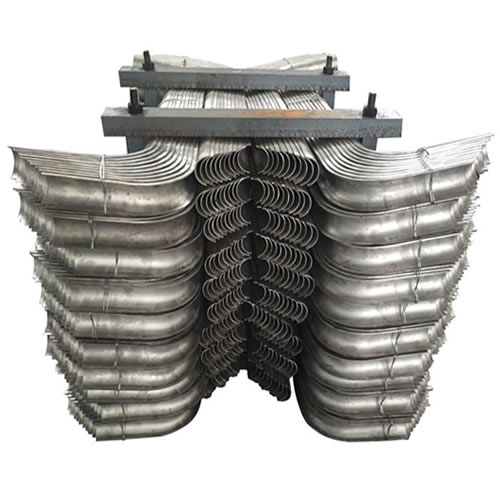
For snap ring fixed installation: Buckle the semi-circular shield on the tube surface, lock C/U snap rings at both ends to prevent shield displacement under flue impact.
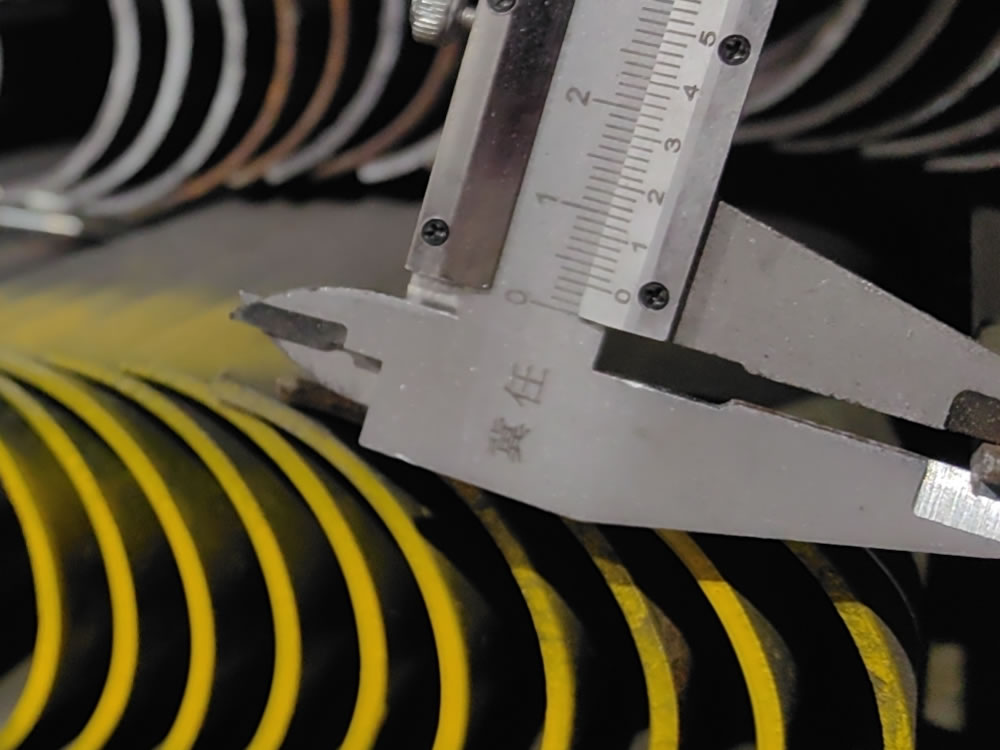
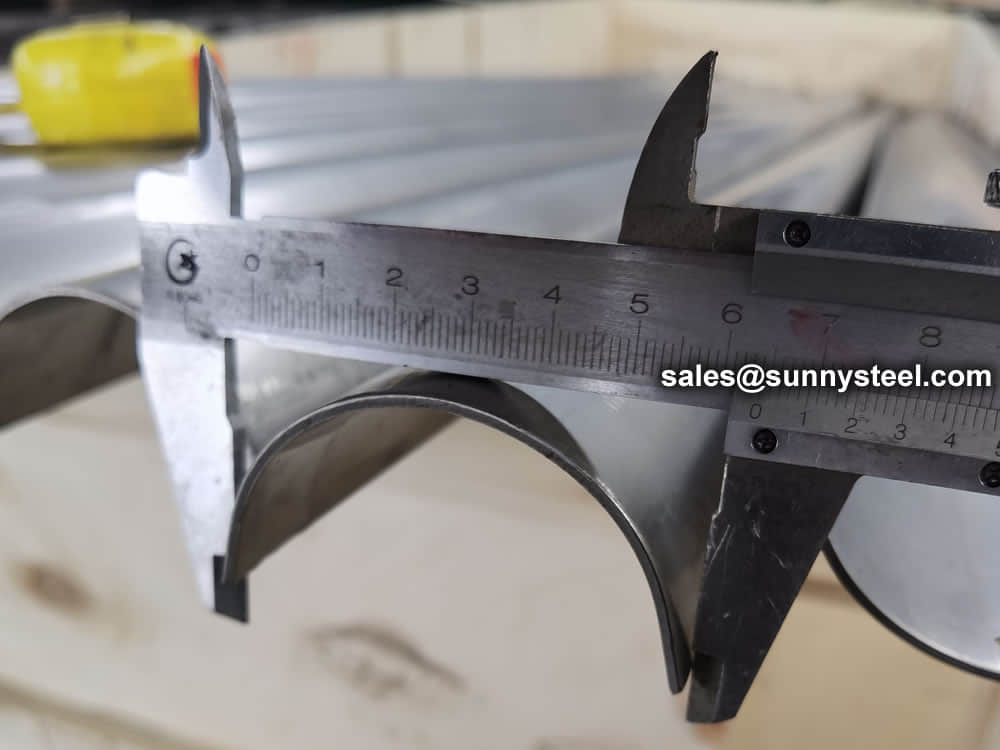
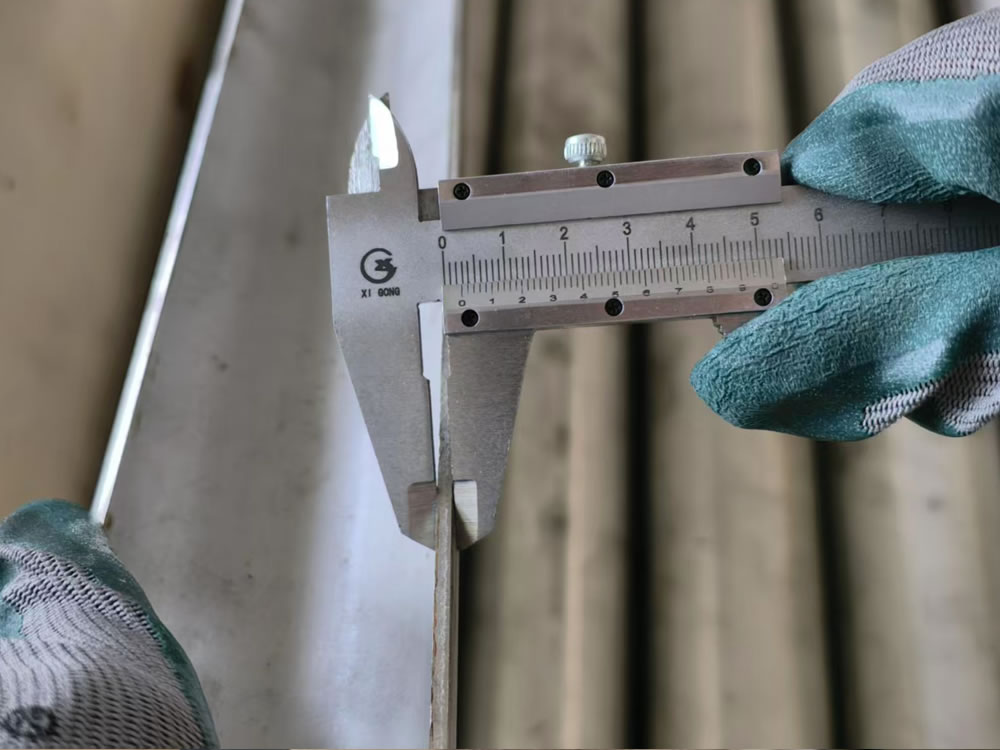
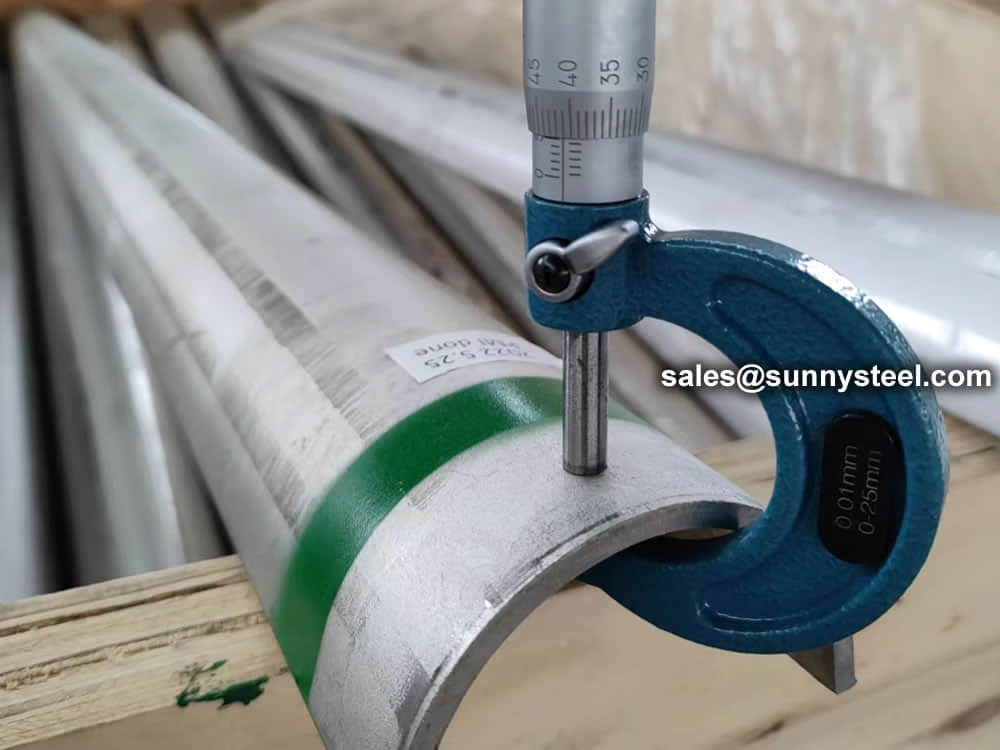
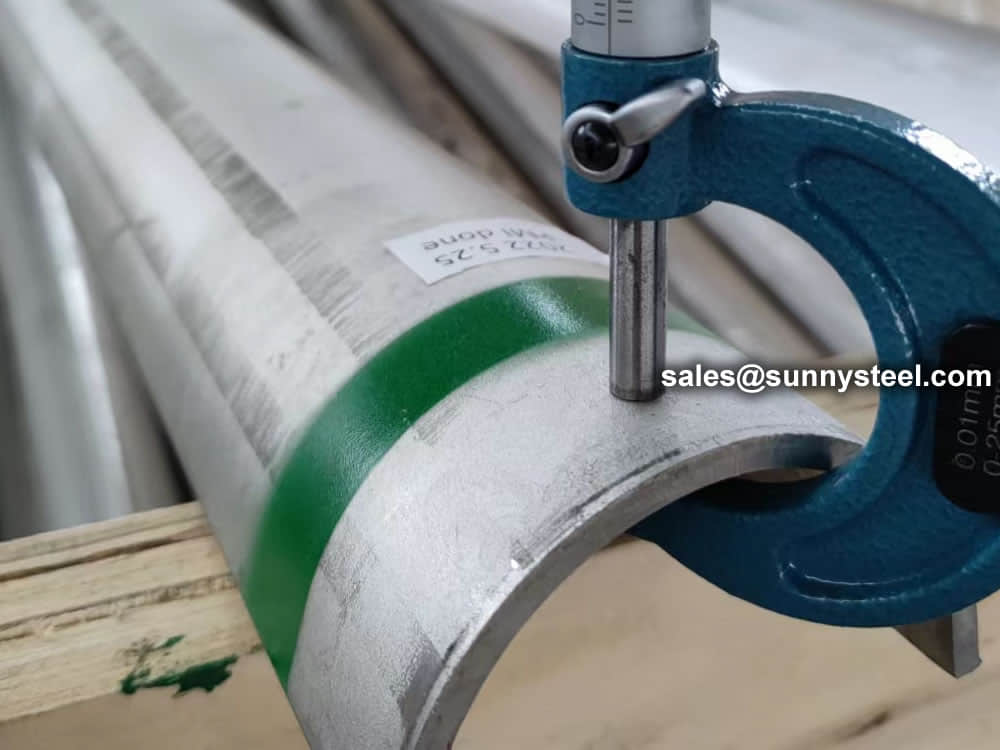
During annual boiler overhaul, check shield thickness thinning and welding crack condition, replace severely abraded shields in advance to avoid tube leakage risk.
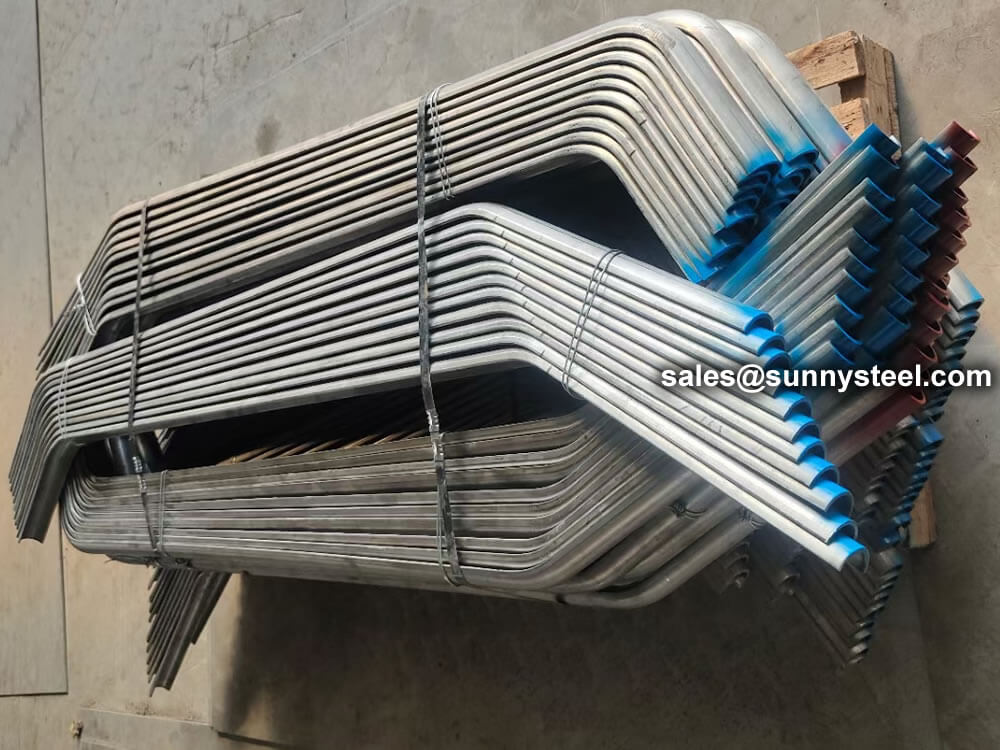
Avoid violent hammer knocking during hoisting to prevent hidden stamping cracks on alloy plate body.